
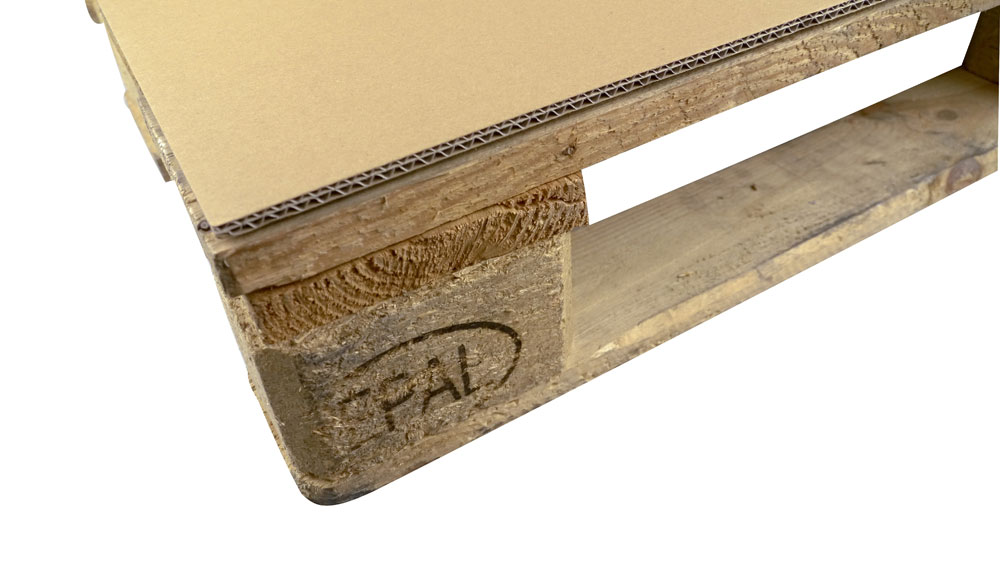
As a storage facility or warehouse owner, dealing with high humidity can be challenging. However, if you find yourself in such a situation, there’s a specialized material that can save the day: cartoncino collato (also known as coated cardboard). In this article, we’ll delve into what it is, its uses and benefits, and how to determine its effectiveness in preventing moisture damage.
What is Cartoncino Collato?
Cartoncino collato is a type of coated cardboard that features a special mixture of water-based cationic adhesive. This unique blend allows for the creation of an impermeable barrier, which prevents water from penetrating the material. The process of making cartoncino collato involves mixing the cationic adhesive with the standard cardboard pulp and then applying it to specific layers of the paper.
The resulting material has a distinct structure that resists absorption of moisture. Unlike traditional cardboard, cartoncino collato’s outer layers are impermeable, while its internal layers remain intact. This characteristic makes it an excellent choice for applications where humidity is a concern.
What Does Cartoncino Collato Serve? And What Are Its Benefits?
Cartoncino collato serves primarily in situations where high humidity can lead to condensation issues. When the air is too humid, water droplets may form on the surface of the carton or even seep into its internal layers. If left unchecked, this moisture can cause irreparable damage to stored products.
To address these challenges, cartoncino collato offers several benefits:
- Material Conservation: By preventing condensation and subsequent moisture damage, cartoncino collato helps reduce material waste.
- Efficient Storage: This specialized material enables more organized and efficient storage systems, saving time and resources for facility managers.
- Product Protection: With cartoncino collato in place, stored products are less likely to suffer from water-related damage, ensuring they remain intact until distribution.
The Prova del COBB 60 Test: Measuring Resistance to Humidity
To verify the effectiveness of cartoncino collato, the COBB 60 test is used. This standardized procedure assesses the material’s ability to resist moisture absorption. Here’s how it works:
- A small sample (approximately a square meter) of cartoncino collato is prepared.
- The sample is then submerged in water for 60 seconds.
- After the treatment, the weight of the sample is measured again.
By comparing the initial and final weights, researchers can calculate the material’s absorption rate, providing valuable insights into its resistance to humidity.
Real-World Applications: Storing Food Products and More
Cartoncino collato plays a vital role in various industries where moisture control is critical. Some common applications include:
- Food Storage: To protect perishable goods from water damage during transportation or storage.
- Pharmaceuticals: To maintain the integrity of sensitive products that are prone to degradation due to moisture exposure.
By understanding the benefits and uses of cartoncino collato, facility managers can make informed decisions about material selection for their storage facilities. This specialized material offers a cost-effective solution for reducing waste, conserving resources, and protecting valuable products from moisture-related damage.
Frequently Asked Questions: Cartoncino Collato and its Applications
- What is the ideal humidity level for using cartoncino collato?
- The COBB 60 test measures resistance to humidity at a relative humidity of 80%. However, the effectiveness of cartoncino collato can vary depending on specific storage conditions.
- Can cartoncino collato be used for other applications beyond food storage?
- Yes, its versatility allows it to be applied in various industries where moisture control is essential.
- How long does the COBB 60 test typically take to complete?
- The entire process, from sample preparation to data analysis, usually takes around an hour.
By addressing common questions and concerns related to cartoncino collato, we can better understand its potential applications and benefits in real-world settings. Whether you’re a storage facility manager or simply looking for ways to optimize your supply chain operations, this specialized material is definitely worth considering.
Additional Considerations: Choosing the Right Cartoncino Collato Type
When selecting cartoncino collato for specific applications, it’s essential to consider various factors:
- Material Strength: Choose a cartoncino collato that balances strength and flexibility based on the stored products’ size and shape.
- Moisture Resistance: Opt for a material with higher moisture resistance levels to ensure effective protection against condensation.
- Cost-Effectiveness: Consider the initial cost of the material and any potential long-term savings due to reduced waste and product damage.
By weighing these factors, you can select the most suitable cartoncino collato type for your storage needs. This will enable you to create an optimal solution that protects valuable products from moisture-related damage while minimizing costs and optimizing resource allocation.
Conclusion: Unlocking the Potential of Cartoncino Collato
Cartoncino collato is a game-changer in various industries, offering unparalleled benefits in terms of material conservation, efficient storage, and product protection. By understanding its composition, effectiveness, and potential applications, facility managers can make informed decisions about selecting the right cartoncino collato for their specific needs.
As we’ve seen, this specialized material is not only an excellent solution for managing high humidity but also a valuable tool for optimizing supply chain operations and reducing waste. Whether you’re dealing with perishable goods or sensitive products, cartoncino collato can help ensure the integrity and safety of your stored inventory.
By embracing the potential of cartoncino collato, you can take a proactive approach to managing moisture-related challenges in your storage facility. This will enable you to create an optimal environment for storing valuable products while minimizing costs and ensuring long-term success.
In conclusion, cartoncino collato is a highly effective solution for addressing moisture-related issues in various industries. By choosing the right material type and considering additional factors like material strength and cost-effectiveness, facility managers can unlock its full potential and create a more efficient, cost-effective storage system that protects valuable products from water damage.


